logo
Supal (Changzhou) Precision Tools Co.,Ltd
Về chúng tôi
Đối tác chuyên nghiệp và đáng tin cậy của bạn.
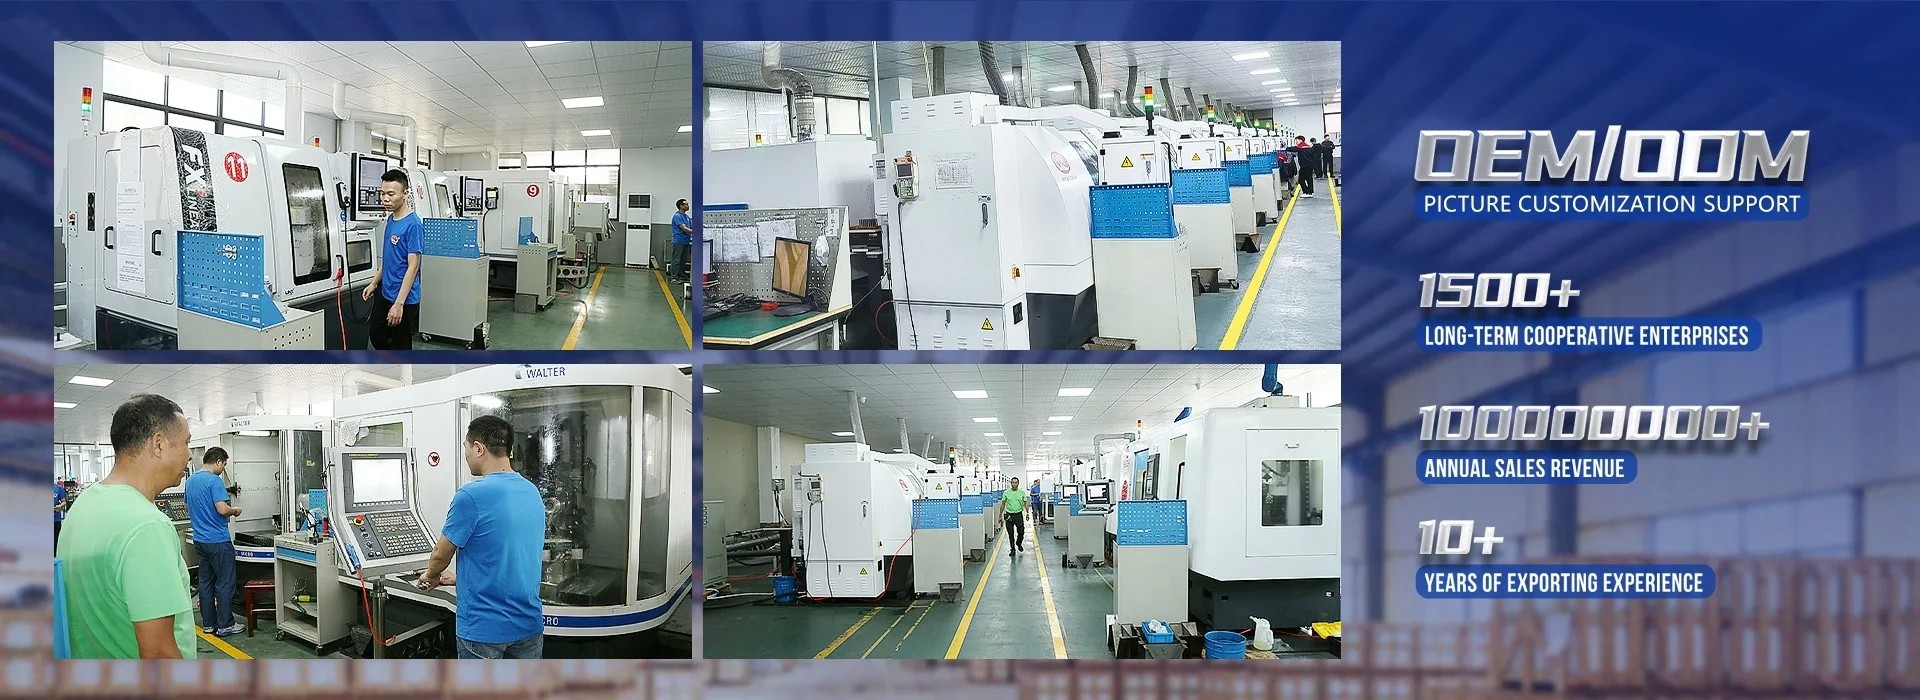
Công ty TNHH Dụng cụ chính xác Supal (Thường Châu) đã tham gia vào thiết kế, sản xuất và kinh doanh các dụng cụ cacbua rắn trong nhiều năm, với tổng vốn đầu tư hơn 10 triệu, và bao gồm một nhóm nhân viên giàu kinh nghiệm.Là một nhà sản xuất dụng cụ chuyên nghiệp, công ty đã trở thành một trong những thành viên ban giám đốc của Hiệp hội Dụng cụ Xiaxiashu Thường Châu. Công ty đã giới thiệu các máy móc của Walter và Schutte của Đức, ANCA của Úc và máy mài dao phay NC năm trục; ngoài ra, công ty còn ...
Tìm hiểu thêm

0

Năm thành lập:

0

Triệu+
Nhân viên

0

Triệu+
Doanh thu hàng năm:
TRUNG QUỐC Supal (Changzhou) Precision Tools Co.,Ltd Chất lượng cao
Con dấu tín nhiệm, kiểm tra tín dụng, RoSH và đánh giá khả năng cung cấp. Công ty có hệ thống kiểm soát chất lượng nghiêm ngặt và phòng thí nghiệm chuyên nghiệp.
TRUNG QUỐC Supal (Changzhou) Precision Tools Co.,Ltd Phát triển
Nhóm thiết kế chuyên nghiệp nội bộ và xưởng máy móc tiên tiến. Chúng tôi có thể hợp tác để phát triển các sản phẩm mà bạn cần.
TRUNG QUỐC Supal (Changzhou) Precision Tools Co.,Ltd Sản xuất
Máy tự động tiên tiến, hệ thống kiểm soát quy trình nghiêm ngặt. Chúng tôi có thể sản xuất tất cả các thiết bị đầu cuối điện ngoài nhu cầu của bạn.
TRUNG QUỐC Supal (Changzhou) Precision Tools Co.,Ltd 100% dịch vụ
Nhập và đóng gói nhỏ tùy chỉnh, FOB, CIF, DDU và DDP. Hãy để chúng tôi giúp bạn tìm ra giải pháp tốt nhất cho tất cả những lo ngại của bạn.

Chất lượng Dụng cụ phay cacbua & dao phay ngón vuông nhà sản xuất

Tìm sản phẩm đáp ứng tốt hơn yêu cầu của bạn.
Các trường hợp và tin tức
Những điểm nóng mới nhất.
Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01

Các lỗ quá lớn: Hướng dẫn giải quyết sự cố
Mài dao cacbua và lỗ quá cỡ: Hướng dẫn khắc phục sự cố Mài dao thường được coi là một thao tác hoàn thiện đơn giản: khoan lỗ, chạy dao mài, và mong đợi kích thước và độ hoàn thiện bề mặt sẽ được cải thiện. Trên thực tế, mài dao cacbua rất nhạy cảm với dung sai, độ thẳng hàng, độ cứng vững, cấp dung dịch làm mát, hình dạng lưỡi cắt và sự ổn định của thông số. Khi bất kỳ biến số nào trong số này bị sai, quy trình có thể tạo ra các vết rung, lỗ quá cỡ, độ tròn kém, lỗ côn, mẻ cạnh, hoặc tuổi thọ dao cụ bị rút ngắn bất ngờ. Đối với các thợ máy CNC, kỹ sư quy trình và kỹ sư mua hàng, điểm mấu chốt là: dao mài không thể khắc phục mọi vấn đề khoan. Dao mài có thể cải thiện một lỗ đã được chuẩn bị, nhưng nó không thể sửa chữa đáng tin cậy một lỗ trước đó bị lệch nghiêm trọng, trầy xước, quá nhỏ, loe miệng, hoặc không ổn định. Hướng dẫn này giải thích cách chẩn đoán các vấn đề về rung dao mài cacbua và dung sai lỗ từng bước, để hành động khắc phục dựa trên chế độ lỗi thay vì phỏng đoán. Tại sao các vấn đề mài dao lại khó chẩn đoán Dao mài cacbua cắt bằng nhiều lưỡi cùng lúc và chỉ loại bỏ một lượng nhỏ vật liệu. Vì thao tác này nhẹ nhàng so với khoan hoặc phay, nhiều xưởng cho rằng mài dao nên dễ dàng bỏ qua. Trên thực tế, dung sai vật liệu nhỏ và mục tiêu dung sai chặt chẽ làm cho quy trình kém khoan dung hơn. Nếu dung sai mài dao quá nhỏ, dao có thể bị cọ xát thay vì cắt. Nếu dung sai quá lớn, các lưỡi cắt có thể bị quá tải. Nếu lỗ khoan không thẳng, dao mài có thể đi theo sai số hiện có hoặc bị buộc phải cắt không đều. Nếu bộ gá hoặc đồ gá thiếu độ cứng vững, rung động nhỏ có thể xuất hiện dưới dạng các đường rung nhìn thấy được bên trong lỗ. Đây là lý do tại sao cùng một dao mài có thể tạo ra độ hoàn thiện tuyệt vời trong một lần gá đặt và thất bại trong một lần gá đặt khác với cùng đường kính lỗ danh nghĩa. Các triệu chứng phổ biến trong mài dao cacbua Các vết rung bên trong lỗ Các vết rung thường xuất hiện dưới dạng các mẫu xoắn ốc lặp lại hoặc giống đa giác trên thành lỗ. Chúng cho thấy dao cụ, bộ gá, phôi, hoặc cấu trúc máy đang rung trong quá trình cắt. Rung động có thể do dung sai quá mức, độ cứng vững không đủ, độ thẳng hàng kém, tốc độ không chính xác, hoặc lỗ trước không ổn định. Lỗ quá cỡ sau khi mài dao Lỗ quá cỡ có thể do dao cụ bị lệch tâm, lệch hàng, áp lực cắt quá mức, giãn nở nhiệt, hoặc phoi bị kẹt giữa dao mài và thành lỗ. Nếu lỗ quá cỡ lặp lại một cách nhất quán, hãy đo độ lệch tâm và kiểm tra tình trạng lỗ trước khi cho rằng đường kính dao mài là sai. Độ hoàn thiện bề mặt kém Độ hoàn thiện bề mặt kém sau khi mài dao có thể do cạnh bám dính, dung dịch làm mát không đủ, phoi bị cắt lại, chuẩn bị lỗ khoan kém, hoặc lưỡi cắt bị mòn. Khi dao mài bị buộc phải loại bỏ vật liệu không đều, độ hoàn thiện bề mặt thường trở nên tồi tệ hơn ngay cả khi dao cụ còn sắc. Tuổi thọ dao cụ ngắn hoặc không nhất quán Nếu một dao mài kéo dài hơn nhiều so với dao khác trong cùng một ứng dụng, hãy xem xét lại việc gá đặt máy, chuẩn bị lỗ, cấp dung dịch làm mát và sự biến đổi vật liệu phôi. Lớp phủ dao cụ và cấp cacbua rất quan trọng, nhưng sự bất ổn định của quy trình thường là điều đầu tiên cần loại bỏ. Mẻ cạnh Mẻ cạnh trên dao mài cacbua thường cho thấy va đập, cắt gián đoạn, dung sai quá mức, vào lỗ kém, hoặc các bao thể cứng trong phôi. Dao mài là dụng cụ hoàn thiện; chúng không được thiết kế để sửa chữa các lỗi khoan lớn hoặc loại bỏ vật liệu nặng. Nguyên nhân gốc rễ 1: Dung sai mài dao không chính xác Dung sai lỗ trước là một trong những biến số quan trọng nhất trong mài dao. Quá ít vật liệu có thể gây cọ xát, sinh nhiệt và hoàn thiện kém. Quá nhiều vật liệu có thể làm quá tải lưỡi cắt và gây rung hoặc mẻ. Không có dung sai phổ quát nào phù hợp với mọi đường kính, vật liệu và thiết kế dao mài. Là nguyên tắc ban đầu, lỗ có đường kính nhỏ thường cần dung sai nhỏ hơn, trong khi lỗ lớn hơn có thể chịu được việc loại bỏ nhiều vật liệu hơn. Tuy nhiên, giá trị chính xác phụ thuộc vào vật liệu phôi, độ sâu lỗ, hình dạng dao cụ, phương pháp làm mát và mục tiêu dung sai. Luôn xác nhận dung sai trên máy và đồ gá thực tế thay vì sao chép giá trị từ một thao tác khác. Khi khắc phục sự cố, hãy so sánh đường kính lỗ khoan thực tế trước khi mài dao với mục tiêu cuối cùng. Nếu kích thước lỗ trước thay đổi từ phôi này sang phôi khác, kết quả mài dao cũng sẽ thay đổi. Nguyên nhân gốc rễ 2: Chất lượng lỗ trước kém Dao mài cần một hướng dẫn ổn định. Nếu lỗ khoan đã bị lệch vị trí, côn, trầy xước, hoặc bị làm cứng bề mặt nghiêm trọng, việc mài dao sẽ khó khăn hơn nhiều. Trước khi đổ lỗi cho dao mài, hãy kiểm tra quy trình khoan. Kiểm tra xem mũi khoan có tạo ra lỗ tròn và thẳng không, liệu phoi có làm trầy xước thành lỗ không, và liệu mũi khoan có bị lệch khi vào lỗ không. Đối với kiểm soát quy trình tạo lỗ, Mũi khoan cacbua và dao mài nên được chọn như một hệ thống, không phải là các dụng cụ không liên quan. Nếu mũi khoan để lại các vết trầy xước phoi nghiêm trọng hoặc kích thước lỗ không nhất quán, dao mài có thể không đủ khả năng kiểm soát để sửa chữa khuyết tật. Hãy cải thiện độ ổn định của quá trình khoan trước, sau đó đánh giá bước mài dao. Nguyên nhân gốc rễ 3: Lệch tâm và lệch hàng Lệch tâm là một trong những cách nhanh nhất để tạo ra lỗ quá cỡ và mài mòn dao không đều. Một lượng nhỏ lệch tâm ở bộ gá hoặc trục chính có thể làm cho một lưỡi cắt làm việc nhiều hơn các lưỡi khác. Điều này tạo ra áp lực cắt không đều, độ tròn kém và tuổi thọ dao cụ ngắn hơn. Kiểm tra độ lệch tâm ở chuôi dao và gần phần cắt khi có thể. Cũng xem xét lại tình trạng bộ gá, độ sạch của đầu kẹp, tình trạng trục chính, và liệu dao cụ có được kẹp với đủ chiều dài tiếp xúc không. Đối với các lỗ chính xác, hệ thống giữ dao cụ quan trọng như chính dao mài. Lệch hàng cũng có thể xảy ra khi dao mài đi vào một lỗ không đồng trục với đường đi của trục chính. Điều này phổ biến khi các thao tác trước đó, đồ gá, hoặc các thiết lập tầm xa gây ra sự biến dạng. Nguyên nhân gốc rễ 4: Tốc độ, tốc độ tiến và độ ổn định cắt Các thông số mài dao nên đủ ổn định để cắt sạch mà không bị cọ xát hoặc rung động. Tốc độ quá cao có thể làm tăng nhiệt và làm trầm trọng thêm rung động ở một số vật liệu. Tốc độ tiến quá thấp có thể gây cọ xát thay vì cắt. Tốc độ tiến quá cao có thể làm quá tải lưỡi cắt và làm hỏng độ hoàn thiện bề mặt. Để khắc phục sự cố, hãy điều chỉnh từng biến số một. Nếu xuất hiện rung động, giảm tốc độ một chút có thể giúp ích, nhưng chỉ khi độ cứng vững và dung sai đã hợp lý. Nếu dao cụ bị cọ xát và sinh nhiệt, việc tăng tốc độ tiến trong phạm vi an toàn đôi khi có thể cải thiện hành động cắt. Thay đổi thông số nên được xác minh thông qua các lần cắt thử trên vật liệu phôi thực tế. Tránh sử dụng các bảng tốc độ và tốc độ tiến chung chung làm giá trị cuối cùng. Hãy coi chúng là tài liệu tham khảo ban đầu và điều chỉnh dựa trên kích thước lỗ, độ sâu, độ cứng vững của máy, dung dịch làm mát và yêu cầu dung sai. Nguyên nhân gốc rễ 5: Dung dịch làm mát và kiểm soát phoi Mặc dù mài dao loại bỏ ít vật liệu hơn khoan, phoi vẫn quan trọng. Các phoi mịn hoặc các hạt bị kẹt bên trong lỗ có thể làm trầy xước thành lỗ và làm hỏng lưỡi cắt. Dung dịch làm mát giúp cuốn trôi phoi, giảm nhiệt và ổn định vùng cắt. Đối với lỗ kín, việc thoát phoi trở nên khó khăn hơn vì phoi có không gian hạn chế để thoát ra khỏi đáy lỗ. Hướng, áp suất và lưu lượng dung dịch làm mát nên được xem xét cẩn thận. Nếu phoi còn sót lại trong lỗ từ quá trình khoan, hãy làm sạch hoặc xả lỗ trước khi mài dao. Nồng độ và lọc dung dịch làm mát cũng quan trọng. Dung dịch làm mát bị nhiễm bẩn có thể mang các hạt mài mòn trở lại vào lỗ, ảnh hưởng đến độ hoàn thiện bề mặt và tuổi thọ dao cụ. Nguyên nhân gốc rễ 6: Hình dạng dao mài và sự phù hợp ứng dụng Các Dao mài cacbua khác nhau được thiết kế cho các ứng dụng khác nhau. Các yếu tố như thiết kế rãnh xoắn, góc dẫn, thiết kế biên, chuẩn bị cạnh và lớp phủ có thể ảnh hưởng đến độ ổn định cắt và thoát phoi. Dao mài cho lỗ thông suốt có thể không hoạt động giống như trong lỗ kín. Dao mài được tối ưu hóa cho nhôm có thể không lý tưởng cho thép không gỉ hoặc vật liệu đã được làm cứng. Dao mài dài có thể yêu cầu sự chú ý thêm về độ cứng vững và độ lệch tâm. Khi thảo luận về một vấn đề dao mài với nhà cung cấp, hãy cung cấp vật liệu phôi, đường kính lỗ trước, dung sai mục tiêu, độ sâu lỗ, tình trạng lỗ thông suốt hay lỗ kín, phương pháp làm mát, thông số hiện tại và ảnh chụp bề mặt lỗ nếu có. Thông tin này giúp xác định xem giải pháp là thay đổi hình dạng, thay đổi thông số hay sửa chữa quy trình. Quy trình khắc phục sự cố thực tế Bước 1: Đo lỗ trước Trước khi kiểm tra lỗ hoàn thiện, hãy đo lỗ khoan hoặc lỗ doa trước khi mài dao. Ghi lại đường kính, độ tròn, độ thẳng nếu có thể, và tình trạng bề mặt. Nếu lỗ trước không ổn định, hãy sửa nó trước. Bước 2: Kiểm tra độ lệch tâm của dao cụ Đo độ lệch tâm trong bộ gá thực tế. Làm sạch chuôi dao, đầu kẹp và bộ gá. Thay thế bộ gá bị hỏng hoặc đầu kẹp bị mòn. Nếu độ lệch tâm giảm và lỗ quá cỡ được cải thiện, dao mài không phải là nguyên nhân chính. Bước 3: Xem xét dung sai So sánh đường kính lỗ khoan thực tế với kích thước dao mài. Nếu dung sai thay đổi giữa các phôi, hãy xác định lý do tại sao thao tác khoan hoặc doa không nhất quán. Bước 4: Kiểm tra phoi và độ hoàn thiện bề mặt Tìm kiếm phoi bị kẹt trong lỗ, vết trầy xước, hoặc vết cọ xát. Nếu xuất hiện vết trầy xước phoi, hãy cải thiện việc cuốn trôi bằng dung dịch làm mát và làm sạch lỗ trước. Bước 5: Điều chỉnh thông số dần dần Thay đổi tốc độ, tốc độ tiến, hoặc dung dịch làm mát từng yếu tố một. Ghi lại kết quả. Tránh thay đổi hình dạng dao cụ và thông số đồng thời trừ khi thiết lập hiện tại rõ ràng là không phù hợp. Bước 6: Xem xét lựa chọn dao cụ Nếu quy trình ổn định nhưng vấn đề vẫn còn, hãy xem xét lại hình dạng dao mài, lớp phủ, kiểu rãnh xoắn và chuẩn bị cạnh. Đối với các ứng dụng gia công và hoàn thiện liên quan, Supal cũng cung cấp Dao phay cacbua cho kế hoạch quy trình CNC rộng hơn. Những sai lầm phổ biến cần tránh Sai lầm 1: Mong đợi dao mài sửa một lỗ xấu Dao mài là dụng cụ hoàn thiện, không phải dụng cụ cứu hộ. Nếu lỗ khoan bị lệch tâm nghiêm trọng, côn, hoặc trầy xước, hãy cải thiện lỗ trước. Sai lầm 2: Bỏ qua độ lệch tâm Độ lệch tâm có thể làm cho dao mài chính xác cắt lỗ quá cỡ. Luôn đo dao cụ trong bộ gá thực tế thay vì cho rằng bản thân dao cụ là sai. Sai lầm 3: Sử dụng dung sai quá ít Quá ít vật liệu có thể gây cọ xát, sinh nhiệt và hoàn thiện kém. Dao cụ phải cắt, không phải đánh bóng vật liệu không đều. Sai lầm 4: Sử dụng dung sai quá nhiều Quá nhiều vật liệu có thể làm quá tải lưỡi cắt và gây rung, mẻ, hoặc độ tròn kém. Sai lầm 5: Thay đổi đường kính dao mài trước khi kiểm tra quy trình Nếu lỗ quá cỡ do lệch tâm, lệch hàng, hoặc rung động, việc thay đổi đường kính dao cụ có thể không giải quyết được vấn đề gốc rễ. Câu hỏi thường gặp Tại sao dao mài cacbua của tôi lại tạo ra lỗ quá cỡ? Các nguyên nhân phổ biến bao gồm lệch tâm, lệch hàng, dung sai quá mức, chất lượng lỗ trước không ổn định, phoi bị kẹt, hoặc hiệu ứng nhiệt. Đo độ lệch tâm và kích thước lỗ trước khi cho rằng đường kính dao mài là không chính xác. Dao mài có thể sửa lỗi lệch tâm của mũi khoan không? Chỉ ở mức độ hạn chế. Nếu lỗ khoan bị lệch vị trí đáng kể hoặc không thẳng, dao mài có thể đi theo sai số hiện có. Hãy cải thiện quy trình khoan hoặc doa trước. Điều gì gây ra rung động trong quá trình mài dao? Rung động có thể do dung sai quá mức, độ cứng vững kém, tốc độ không chính xác, phần nhô ra của dao cụ dài, hình dạng lỗ trước không ổn định, hoặc độ thẳng hàng kém giữa trục chính và lỗ. Tôi có nên giảm tốc độ hoặc tốc độ tiến để dừng rung dao mài không? Đôi khi giảm tốc độ giúp ích, nhưng nó không phải lúc nào cũng là giải pháp đầu tiên. Hãy kiểm tra độ lệch tâm, dung sai, độ cứng vững của bộ gá và chất lượng lỗ trước. Tốc độ tiến quá thấp cũng có thể gây cọ xát. Tôi nên cung cấp thông tin gì khi yêu cầu hỗ trợ khắc phục sự cố dao mài? Cung cấp vật liệu phôi, đường kính lỗ trước, đường kính và dung sai mục tiêu, độ sâu lỗ, tình trạng lỗ thông suốt hay lỗ kín, phương pháp làm mát, tốc độ/tốc độ tiến hiện tại, phần nhô ra của dao cụ, loại bộ gá, và ảnh chụp bề mặt lỗ hoặc dao mài bị mòn. Kết luận Rung dao mài cacbua, lỗ quá cỡ và tuổi thọ dao cụ ngắn thường là các vấn đề về quy trình, không chỉ là vấn đề về dao cụ. Chuỗi khắc phục sự cố hiệu quả nhất là đo lỗ trước, kiểm tra độ lệch tâm, xem xét dung sai, kiểm tra các vết trên bề mặt và điều chỉnh thông số từng biến số một. Nếu bạn đang gặp phải dung sai lỗ không ổn định, các vết rung, hoặc tuổi thọ dao mài ngắn, Liên hệ Supal với vật liệu phôi, tình trạng lỗ trước, dung sai mục tiêu, thông số hiện tại và ảnh chụp lỗi. Supal có thể giúp đánh giá xem nguyên nhân gốc rễ là dung sai, độ lệch tâm, dung dịch làm mát, hình dạng dao mài, hay độ ổn định quy trình tổng thể.

2026

09/29